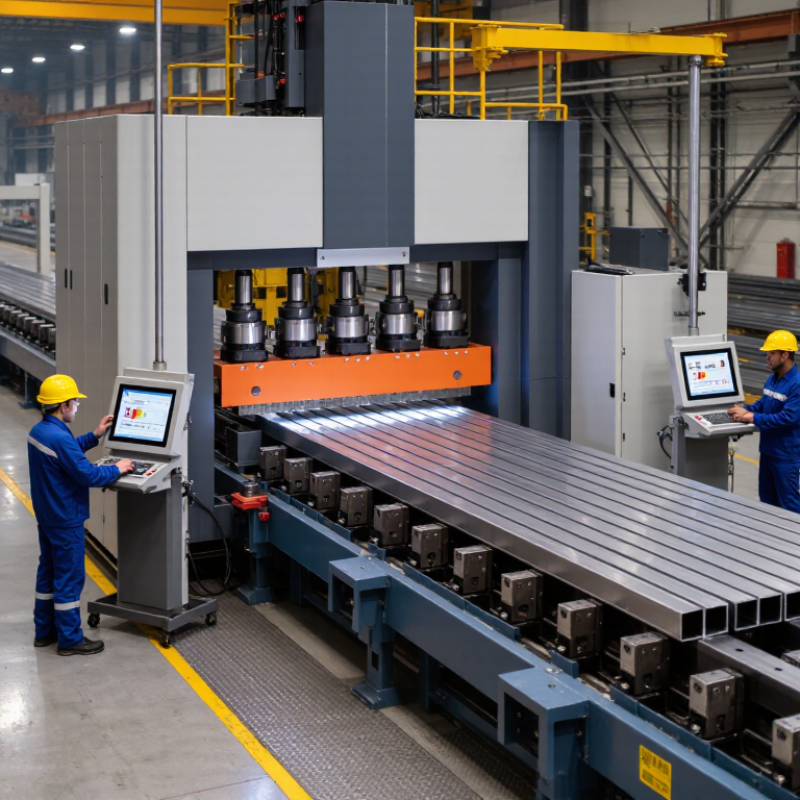
Entry Level
Compact Strut Channel Roll Former | Small workshops, maintenance contractors, prototype orders, and low-volume production with frequent product changes. | Carbon steel or galvanized steel
Approximately 0.80–2.00 mm | Approximately 8–18 m/min | Usually one profile family, such as 41 × 21 mm or 41 × 41 mm. | Limited
Stand-alone punching or manual drilling is commonly used. | Manual or semi-automatic feeding, cutting, and length setting. | Prioritize compact layout, quick tooling adjustment, low setup cost, and easy operator access. |
Flexible
Multi-Profile Roll Forming Line | General fabrication plants producing several channel sizes or switching between solid and slotted profiles. | Galvanized, pre-galvanized, or mild steel
Approximately 0.80–2.50 mm | Approximately 12–25 m/min | Several compatible widths and heights, subject to roll-tool design and machine adjustment range. | Available
In-line punching can produce repeated round, square, or elongated slots. | Automatic length control with servo feeding and programmable recipes. | Confirm changeover time, tooling interchangeability, profile tolerances, and the maximum number of product recipes. |
High Output
Continuous Roll Former with In-Line Punching | Medium- to high-volume production of slotted channels for electrical, mechanical, solar, and construction applications. | Galvanized or coated steel
Approximately 1.00–2.50 mm | Approximately 18–35 m/min, depending on hole spacing and profile complexity. | Standard channel sections with continuous or repeating slot patterns. | Integrated
Servo-driven punching before or after roll forming, depending on the profile and hole pattern. | Automatic decoiler, straightener, servo feeder, punching press, flying cut-off, and PLC control. | Evaluate punching accuracy at line speed, press capacity, die life, scrap handling, and synchronization between punching and forming. |
Heavy Duty
Thick-Gauge Strut Channel Machine | Structural support systems, industrial frames, heavy cable trays, pipe supports, and applications requiring higher load capacity. | Mild steel, galvanized steel, or stainless steel
Approximately 1.50–4.00 mm | Approximately 8–20 m/min | Deeper or wider channels, reinforced lips, and heavier structural profiles. | Available
Requires correctly sized punching equipment and hardened tooling for thicker material. | Automatic feeding and cutting with reinforced forming stands and closed-loop length control. | Check motor torque, shaft diameter, stand rigidity, roll material, punching force, and cut-off performance at maximum thickness. |
Custom Production
Special-Profile Roll Forming Line | Manufacturers producing non-standard channels, custom lips, special mounting holes, or application-specific profiles. | Material and thickness selected according to the engineered profile
Commonly 0.80–3.00 mm | Approximately 6–25 m/min | Custom dimensions, formed edges, stiffening ribs, and special return lips. | Project Dependent
Punching, notching, embossing, or pre-cutting may be integrated after engineering review. | Servo-controlled line with recipe management and application-specific sensors. | Require profile drawings, material samples, tolerance targets, tooling simulations, and a documented acceptance test. |
Fully Automated
Integrated Coil-to-Length Production Cell | Large plants seeking reduced labor, stable repeatability, automatic packing, and continuous multi-shift operation. | Galvanized, pre-painted, or stainless steel
Approximately 0.80–3.00 mm | Approximately 15–40 m/min, subject to profile and punching requirements. | Multiple standard profiles supported through dedicated or quick-change tooling systems. | Fully Integrated
Programmable hole patterns, cut lengths, batch counts, and production sequences. | Automatic coil loading, servo control, in-line inspection, cut-to-length, stacking, and data monitoring. | Compare total cost of ownership, maintenance access, sensor redundancy, software support, safety systems, and spare-parts availability. |
Short-Run
Pre-Cut Blank Roll Forming System | Job shops and plants producing short batches where different blank lengths or reduced coil waste are important. | Mild, galvanized, or stainless steel
Approximately 0.80–2.50 mm | Approximately 8–22 m/min | Standard and semi-custom channels with controlled blank length. | Optional
Holes may be punched in the blank before forming or added in a separate operation. | Semi-automatic loading with programmable blank feeding and cut-length control. | Select this type when material utilization and short changeover time are more important than maximum throughput. |


 Close