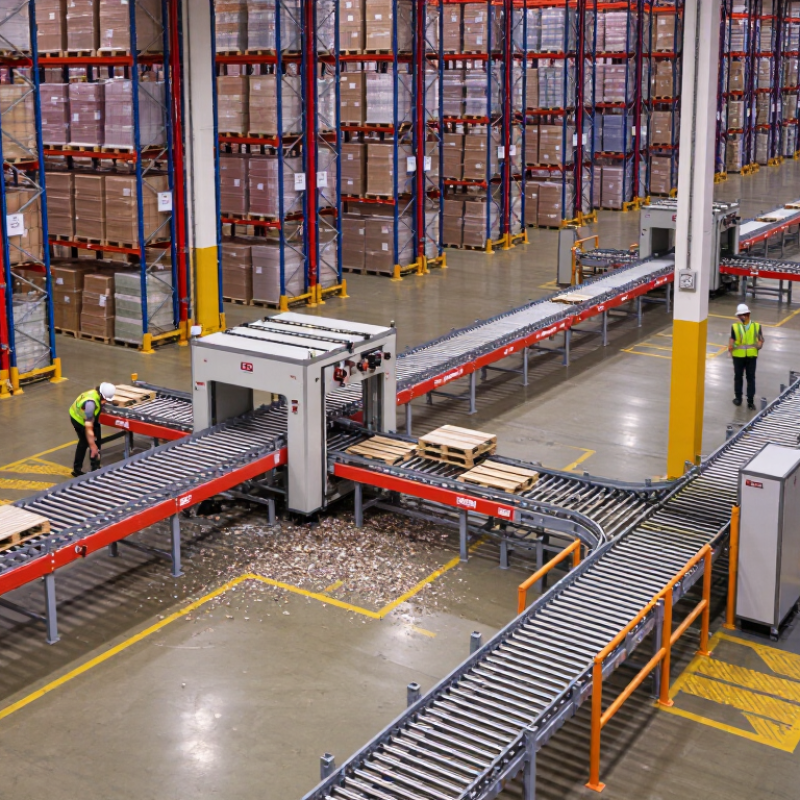
| 1 | Balance conveyor zones | Use zero-pressure accumulation with independent motorized zones so pallets stop without contacting one another. | Zone occupancy, blocked time, release interval, and pallet spacing. | Maintain approximately 10–20% spare capacity during normal peak periods. | Reduces congestion, product contact, and repeated starts and stops. |
| 2 | Install sensors at decision points | Place photoelectric or laser sensors at transfers, accumulation zones, merges, and pallet-stop positions. | Detection response time, missed detections, blocked sensors, and false triggers. | Use response times below 100 milliseconds where high-speed accumulation is required. | Improves pallet tracking and prevents avoidable stoppages caused by poor detection. |
| 3 | Automate identification and routing | Combine barcode or RFID identification with programmable logic controls and automatic divert stations. | Read rate, misroute rate, scan-to-divert time, and exception volume. | Design for a barcode read rate of at least 99.5% under normal operating conditions. | Lowers manual keying, sorting errors, and unnecessary pallet recirculation. |
| 4 | Use variable-speed control | Apply variable-frequency drives and speed profiles that adjust conveyor velocity to demand and downstream availability. | Motor speed, queue length, cycle time, energy consumption, and downstream availability. | Operate only as fast as the slowest active process can safely receive pallets. | Reduces unnecessary energy use, mechanical wear, and accumulation pressure. |
| 5 | Monitor throughput in real time | Connect conveyor controls to a warehouse management or supervisory monitoring system with live dashboards. | Pallets per hour, utilization, downtime minutes, queue size, and mean time between stops. | Track throughput by shift and compare actual output with the planned rate. | Makes bottlenecks visible before they become extended operational delays. |
| 6 | Adopt condition-based maintenance | Use vibration, temperature, current, and runtime monitoring for motors, gearboxes, rollers, and bearings. | Unplanned downtime, fault frequency, vibration trend, motor current, and mean time to repair. | Review trend alarms before measured values reach equipment limits. | Supports planned repairs and reduces the likelihood of sudden conveyor failures. |
| 7 | Design for safe and efficient pallet flow | Use guarded transfer points, presence detection, emergency-stop circuits, adjustable guides, and standardized pallet dimensions. | Transfer faults, damaged pallets, emergency stops, safety events, and manual interventions. | Keep pallet overhang, load height, and weight within documented conveyor design limits. | Improves uptime, protects workers and goods, and reduces rework caused by unstable loads. |


 Close