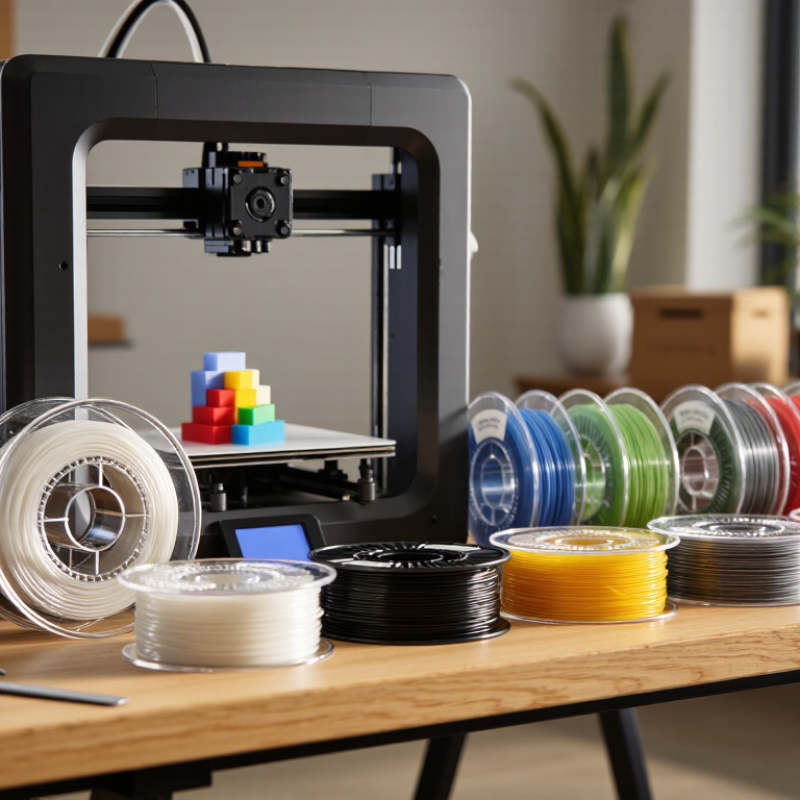
| PLA | 190–220°C | 0–60°C | Easy to print, rigid, and generally low-warping; limited heat resistance. | Prototypes, models, décor, and everyday indoor objects. | Can soften in hot environments; not ideal for sustained outdoor exposure or high temperatures. |
| PETG | 220–250°C | 70–90°C | Tough and somewhat flexible, with good layer adhesion and better moisture resistance than PLA. | Functional parts, brackets, containers, and outdoor items with moderate demands. | May string during printing; can adhere strongly to some build surfaces. |
| ABS | 230–260°C | 90–110°C | Impact-resistant and more heat-resistant than PLA; can be post-processed with acetone. | Enclosures, durable components, and parts exposed to moderate heat. | Prone to warping; an enclosure and good ventilation are recommended because printing can release irritating fumes. |
| ASA | 240–260°C | 90–110°C | Durable and weather-resistant, with strong resistance to UV exposure compared with ABS. | Outdoor housings, fixtures, and parts exposed to sunlight or changing weather. | Can warp and benefits from an enclosure; use good ventilation while printing. |
| TPU | 210–240°C | 30–60°C | Flexible, elastic, and abrasion-resistant; softness depends on the material’s hardness rating. | Protective covers, flexible hinges, grips, and vibration-damping parts. | Print slowly; flexible filament can be difficult to feed through some extruder setups. |
| Nylon (Polyamide) | 240–290°C | 70–100°C | Tough, wear-resistant, and relatively flexible under load. | Gears, fasteners, hinges, and functional parts subject to repeated movement. | Absorbs moisture readily; dry before printing and store in a sealed, dry environment. Warping can occur. |
| Polycarbonate (PC) | 260–310°C | 90–120°C | High impact strength and heat resistance; properties vary considerably by formulation. | Strong functional parts and components that need to withstand elevated temperatures. | Requires a high-temperature-capable printer; an enclosure and dry filament help reduce warping and print defects. |
| PVA (Water-Soluble Support) | 190–220°C | 45–60°C | Dissolves in water, making it useful as removable support material for complex shapes. | Dual-extrusion prints with enclosed cavities or hard-to-reach support structures. | Highly moisture-sensitive; keep it dry and confirm compatibility with the main printing material. |
| HIPS (High-Impact Polystyrene) | 220–250°C | 90–110°C | Lightweight, impact-resistant, and soluble in limonene; often used as removable support. | Support structures for compatible materials and lightweight prototypes. | Can warp; dissolving supports requires limonene and appropriate handling. |
| Wood-Filled PLA | 190–220°C | 0–60°C | PLA blended with wood particles for a matte, wood-like appearance and texture. | Decorative models, ornaments, and display pieces. | Can clog small nozzles; filled filaments may wear soft brass nozzles over time. Print settings depend on the blend. |


 Close