How to Choose a Metal Detector for Biscuits?
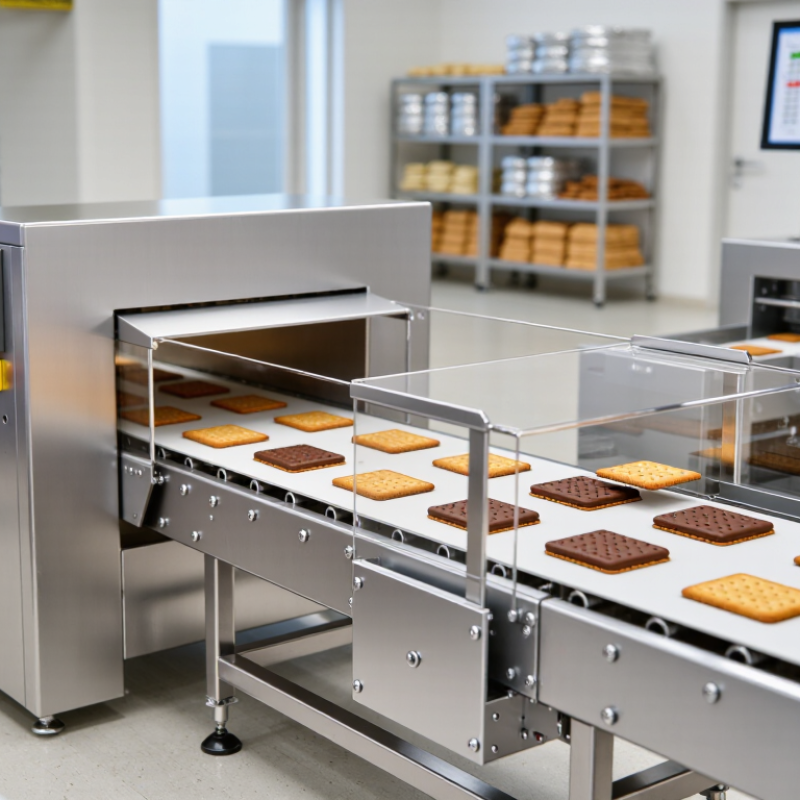
Choosing the right Metal Detector for Biscuits requires more than comparing prices or detection ranges. Biscuit production combines dry crumbs, variable moisture, metal packaging, and fast conveyor movement. Each detail can affect inspection accuracy.
Ian Atkinson, an experienced food inspection specialist, explains, “A detector is only as good as the product effect it can control.” This practical view matters on a busy biscuit line. A machine may perform well during a showroom test, yet struggle with warm products or changing recipes. Real production trials are essential.
Begin by examining the biscuit itself. Measure its size, temperature, moisture, salt content, and packaging format. A chocolate-coated biscuit may behave differently from a plain cracker. Product effect can create unstable signals, especially when ingredients change between batches. The detector should support automatic product setup, reliable signal processing, and simple sensitivity adjustment.
Consider the conveyor speed and available installation space. The reject system must remove suspect products without damaging nearby biscuits. It should also include clear alarms, secure access, and easy cleaning surfaces. Validation tests should use certified test pieces at realistic production conditions. Record every result.
No choice is perfect.
It is tempting to select the most sensitive model. That can be a mistake if false rejects interrupt production. Operators need understandable controls and consistent procedures. Maintenance teams need quick access to belts, sensors, and reject mechanisms. A dependable Metal Detector for Biscuits balances detection performance, hygiene, usability, and long-term operating cost. Careful testing reveals weaknesses early. Sometimes, the first decision needs revision. That is not failure; it is sound engineering.
Define Biscuit Contamination Risks: Ferrous, Non-Ferrous, and Stainless Steel
How to Choose a Metal Detector for Biscuits?
Define Biscuit Contamination Risks: Ferrous, Non-Ferrous, and Stainless Steel
Biscuit lines face contamination risks from equipment wear, maintenance work, and damaged packaging materials. An effective detector must identify ferrous, non-ferrous, and stainless-steel fragments without rejecting good products unnecessarily. In practical production checks, ferrous metal is usually the easiest target to detect. It may come from worn screws, blades, or conveyor components. Non-ferrous metals, such as aluminium or copper, can be more difficult to detect because they create weaker signals.
Stainless steel needs special attention. Its low magnetic response and electrical properties can reduce detection sensitivity. Small stainless-steel pieces may pass unnoticed if the system is adjusted only for iron. Product characteristics also matter. Moisture, salt, temperature, biscuit size, and orientation can influence the signal. Test the detector with real biscuits, not only test samples. A dry biscuit may behave differently from one containing chocolate, cream, or a moist filling.
Choose equipment that supports separate test standards for all three metal types. The aperture should fit the product flow closely, while the reject system should remove suspect biscuits cleanly. Operators should record checks at start-up, after product changes, and during long runs. No setting is perfect. I have seen teams focus on ferrous detection and overlook stainless steel after cleaning or repairs. That gap deserves honest review, repeated testing, and better operator training.
Select Multi-Frequency Technology for Low-Moisture Biscuit Products
How to Choose a Metal Detector for Biscuits?
Biscuits are low-moisture products, but they can still challenge metal detection. Salt, sugar, fat, and baked product temperature may create unstable product signals. Multi-frequency technology helps by scanning across several frequencies and selecting the clearest response for each product. This can improve detection stability for ferrous, non-ferrous, and stainless-steel fragments.
Start with real production samples, not only clean test pieces. Test warm biscuits, filled biscuits, and products after packaging. Check the smallest certified test spheres at the actual line speed. A practical trial should also include rejected packs, belt stops, and product changeovers. Small details matter. Poor alignment can reduce performance.
The World Health Organization reports that contaminated food causes about 600 million illnesses and 420,000 deaths globally each year. This figure covers all food hazards, not metal alone, but it shows why validated controls matter. The Codex General Principles of Food Hygiene recommends preventive systems and verified control measures for physical hazards. Choose equipment with automatic monitoring, secure reject confirmation, and clear audit records. Multi-frequency is not magic. Product testing may reveal that one frequency performs better than another, and that result deserves careful review rather than a confident assumption.
Verify Reject Accuracy and HACCP Compliance Through Routine Testing
How to Choose a Metal Detector for Biscuits?
Choosing a metal detector for biscuits requires more than checking sensitivity numbers. The product size, belt speed, packaging, and biscuit recipe can affect detection performance. Dry biscuits usually create limited product effect, but fillings, salt, moisture, or inclusions may change the signal. Select an aperture that fits the largest product safely. A smaller opening often improves sensitivity. Confirm that the system can detect ferrous, non-ferrous, and stainless-steel test pieces at the planned production speed.
Reject accuracy deserves equal attention. A detector may identify contamination correctly, yet the reject device can still fail. Test the full process, including the sensor, alarm, conveyor stop, and reject confirmation. Place traceable test pieces inside real biscuit packs, not only beside the product. Check them at the centre and edges of the aperture. Small details matter. Record the product code, test size, time, operator, and result. Keep rejected items separated and clearly identified.
Routine testing supports HACCP verification and provides evidence that controls remain effective. Test at start-up, after product changes, following cleaning, and after unexpected stoppages. Repeat checks during production at a defined frequency. If one test fails, stop the affected line and investigate before release. Possible causes include speed changes, poor alignment, electrical interference, or an obstructed reject mechanism. A common mistake is trusting yesterday’s result. Conditions change. Review records regularly, and adjust the procedure when experience exposes a weak point. Perfect routines are rare. Honest records are essential.
 Close