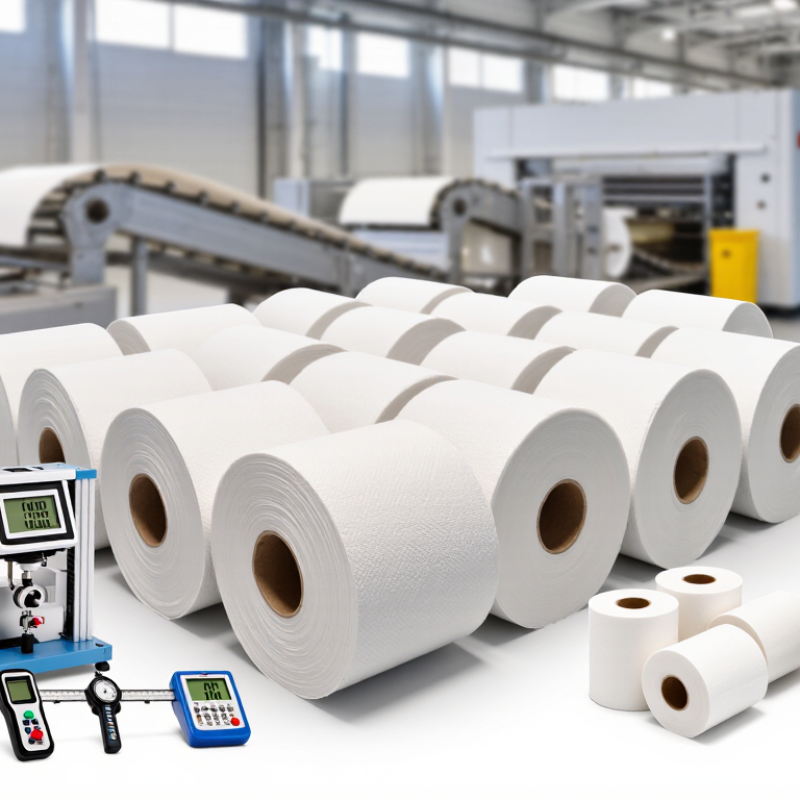
| Basis Weight | Common tissue grades are approximately 13–40 g/m² per ply. The buyer’s tolerance should normally be defined around the agreed nominal value. | Condition samples at 23 ± 1°C and 50 ± 2% relative humidity, then determine grammage according to ISO 536 or an equivalent standard. | Controls converting yield, roll weight, product thickness, cost calculations, and consistency between shipments. |
| Moisture Content | A practical receiving target for many tissue grades is about 4–8%, subject to furnish, machine conditions, and the agreed specification. | Oven-dry moisture measurement in accordance with ISO 638, or a calibrated moisture analyzer verified against the oven method. | Excess moisture can increase freight weight, cause telescoping or blocking, and affect converting performance. |
| Machine-Direction Tensile Strength | Set the minimum value according to the converting line, ply count, basis weight, and end use. The machine direction generally requires higher strength than the cross direction. | Strip tensile testing using ISO 12625-4 or a comparable tissue-paper tensile method; report strength and elongation. | Insufficient strength can lead to web breaks, downtime, and waste during unwinding, embossing, folding, or perforating. |
| Cross-Direction Tensile and Wet Strength | Use a wet-strength requirement only when the finished application needs resistance to disintegration when wet. Dry and wet targets should be agreed separately. | Test dry tensile and wet tensile using applicable ISO 12625 procedures or an agreed laboratory method. | Balances user performance with flushability, repulpability, and environmental requirements. |
| Bulk and Caliper | Specify caliper or bulk together with basis weight. A higher bulk generally improves softness and absorbency but may reduce roll length at the same roll diameter. | Measure thickness under a controlled pressure using ISO 12625-3 or an equivalent method; calculate bulk as thickness divided by grammage. | Supports accurate roll-capacity planning, packaging design, and finished-product appearance. |
| Water Absorption | Define an absorption target based on whether the material is intended for facial, bath, napkin, towel, or industrial tissue applications. | Use a specified water-absorption or sinking-time method, such as ISO 12625-8, and keep sample size and conditioning consistent. | Absorption directly affects consumer perception, sheet consumption, and suitability for the intended converting category. |
| Brightness, Color, and Shade | Define the measurement system and tolerance. ISO brightness and CIE whiteness are different indicators and should not be used interchangeably. | Measure with a calibrated optical instrument using ISO 2470-1 or the agreed color and brightness standard. | Prevents visible shade variation between parent rolls, production lots, and converting locations. |
| Softness and Surface Feel | Use a defined instrumental softness target or a controlled sensory reference sample. Softness should be evaluated together with strength and bulk. | Conduct panel comparison under controlled conditions or use an accepted tissue softness instrument and reference board. | Instrumental results alone may not predict user perception; a retained reference sample improves global lot approval. |
| Reel Dimensions and Core | Specify roll width, maximum diameter, core inside diameter, core material, winding direction, roll hardness, and allowable width tolerance. | Verify dimensions with calibrated gauges and inspect roll hardness, edge alignment, core damage, and telescoping before shipment. | Ensures compatibility with unwinders, slitters, embossers, rewinding machines, and automated material handling. |
| Web Cleanliness and Defects | No oil, dirt, adhesive, metal particles, plastic fragments, excessive dust, holes, wrinkles, edge cracks, or severe formation streaks. | Use visual inspection under suitable lighting, defect mapping, and agreed sampling based on ISO 2859-1 or a documented quality plan. | Reduces complaints, line stoppages, contamination risk, and finished-product rejection. |
| Fiber and Recycled Content | State whether the furnish is virgin fiber, recycled fiber, or a defined blend. If recycled content is claimed, specify the minimum percentage and calculation basis. | Review supplier declarations, pulp documentation, chain-of-custody records where applicable, and conduct periodic laboratory or third-party verification. | Improves traceability and supports environmental claims, import documentation, and customer compliance requirements. |
| Chemical and Product Safety | Define limits for restricted substances, optical brighteners, fragrances, dyes, microbiological contamination, and food-contact or cosmetic-contact requirements where relevant. | Request a current test report from a competent laboratory and review the applicable destination-market regulations before approval. | Regulatory requirements vary by destination and end use; documentation gaps can delay customs clearance or market release. |
| Packaging and Export Protection | Use moisture-resistant wrapping, protected roll edges, secure palletization, visible lot identification, and packaging suitable for the expected transport route. | Inspect packaging before loading and record container condition, pallet count, roll count, gross weight, lot number, and loading photographs. | Protects hygroscopic tissue from humidity, compression, contamination, and handling damage during long-distance transportation. |
| Batch Consistency and Documentation | Every shipment should include a lot number, certificate of analysis, production date, roll specifications, test results, and nonconformance procedure. | Compare pre-shipment samples, certificate data, and arrival inspection results using an approved quality agreement. | Creates an auditable basis for supplier approval, claims management, corrective actions, and repeat purchasing. |


 Close