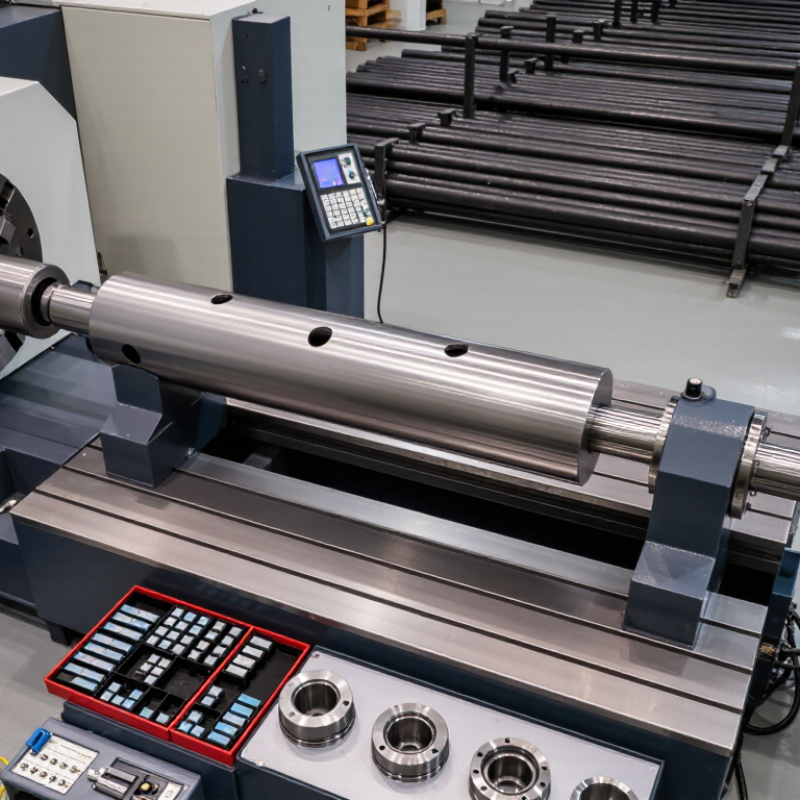
| Steel hydraulic cylinder tube | Inside diameter: 40–150 mm
Length: 1–6 m | Low to medium; frequent changes in tube size or length | Horizontal machine with adjustable supports, through-bore capability, and a stroke suited to the longest part | Confirm maximum workpiece length, support spacing, bar rigidity, and the required bore finish. Long tubes need adequate support to limit deflection. |
| Cast iron engine or compressor cylinder | Inside diameter: 70–180 mm
Length: 100–500 mm | Medium to high; repeated parts and stable process conditions | Vertical or horizontal machine with repeatable fixturing and programmable stroke and dwell settings | Check casting variation, bore alignment, stock allowance, and whether the machine can consistently produce the specified crosshatch and geometry. |
| Stainless steel process tube | Inside diameter: 25–100 mm
Length: 0.5–4 m | Low to medium; material grades and dimensions may vary | Horizontal machine with adjustable tooling and controlled honing-fluid delivery | Verify abrasive compatibility, coolant filtration, corrosion control, and the ability to prevent heat buildup or surface damage. |
| Aluminum alloy sleeve or housing | Inside diameter: 20–80 mm
Length: 50–400 mm | Medium to high; often batch production | Compact vertical or horizontal machine with accurate workholding and adjustable pressure | Use a process suited to the alloy and required finish. Check clamping force to avoid distorting thin walls and confirm reliable chip and abrasive removal. |
| Hardened steel hydraulic or precision component | Inside diameter: 10–60 mm
Length: 100–1,000 mm | Low to medium; tight tolerances or high-value parts | Precision machine with rigid tooling, controlled feed, and in-process or frequent bore measurement | Assess hardness, initial bore condition, stock removal, roundness and straightness requirements, and the measurement method used for process verification. |
| Long, small-diameter bore in steel or alloy | Inside diameter: 8–30 mm
Length: 0.5–3 m | Low to medium; setup stability is especially important | Deep-stroke horizontal configuration with a suitably long honing tool and support for the workpiece and tool | Check the bore length-to-diameter ratio, tool reach and stiffness, alignment, coolant access, and the risk of tool deflection or vibration. |
| Mixed-material job shop work | Inside diameter: 15–200 mm
Length: 100 mm–6 m | Low volume; frequent changes in part family | Flexible machine with interchangeable tooling, adjustable supports, and a broad usable stroke and diameter range | Compare the actual part range with the machine’s rated limits. Consider changeover time, tooling availability, operator access, and the number of setups required. |



 Close