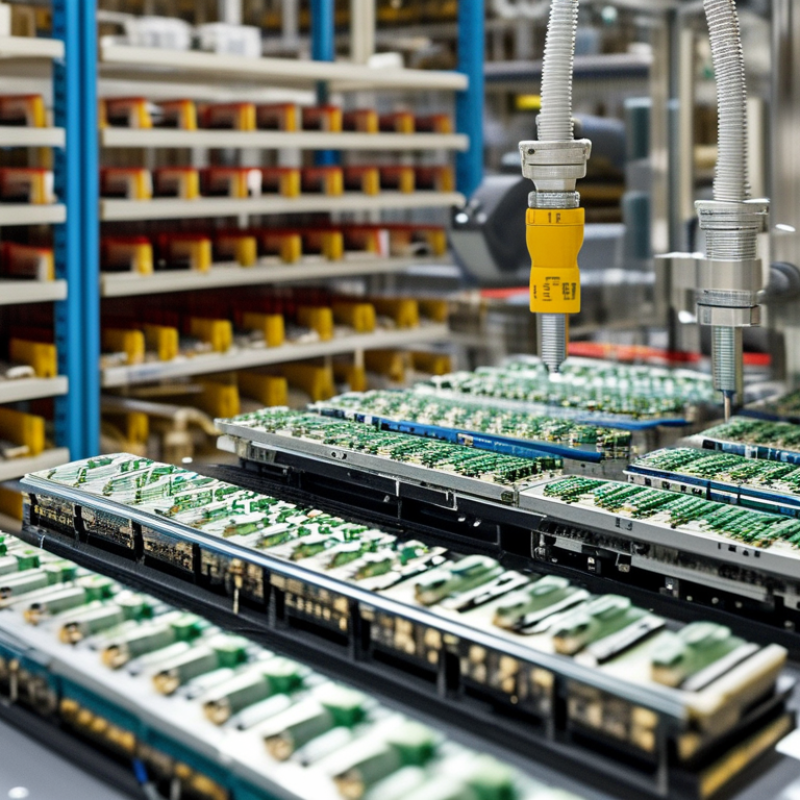
| 0.4 mm-pitch SMT placement | Confirm that the production line has placed fine-pitch components at 0.4 mm on comparable assemblies. | Documented experience with 0.4 mm-pitch devices, suitable feeders, vision alignment, controlled solder paste printing, and verified placement accuracy. | Anonymized production records, sample images, machine capability statement, and first-article inspection report. | 20% |
| BGA assembly | Check experience with BGA package assembly, reflow profiling, pad design review, and post-reflow inspection. | Controlled reflow profiles for the actual board stack-up and component mix, plus a documented method for detecting hidden solder joints. | Thermal profiles, BGA inspection samples, process-control plan, and X-ray availability or qualified access. | 15% |
| Solder paste inspection (SPI) | Verify that SPI is used after printing rather than relying only on visual inspection. | Measurement of paste volume, height, area, offset, and bridging risk with traceable inspection data and defined alarm limits. | Sample SPI reports, calibration records, inspection-frequency rules, and corrective-action examples. | 15% |
| Automated optical inspection (AOI) | Confirm AOI coverage for component presence, polarity, placement, solder bridging, and visible solder-joint conditions. | AOI programs validated against the approved BOM and layout, with false-call control and repair-loop records. | AOI program screenshots, defect-classification reports, sample images, and verification procedures. | 10% |
| X-ray inspection for hidden joints | Determine how the supplier inspects BGA, bottom-terminated, and other concealed solder connections. | Defined 2D or 3D X-ray inspection criteria based on package type, defect risk, and customer requirements. | X-ray capability details, sample images, inspection plan, and operator qualification records. | 10% |
| Stencil and solder-paste process | Review stencil design, aperture strategy, paste storage, thawing, mixing, and time-out control. | Process controls matched to fine-pitch and thermal-pad requirements, with documented paste shelf-life and floor-life management. | Stencil drawings, paste-control log, cleaning schedule, and print-process work instructions. | 10% |
| Reflow and thermal-process control | Check whether profiles are measured on representative boards and maintained within component and paste limits. | Profile approval before production, documented recipe control, and requalification after significant material or equipment changes. | Profile graphs, recipe-approval records, oven-maintenance logs, and change-control records. | 8% |
| Traceability and data retention | Verify lot, date-code, operator, machine, material, and inspection-result traceability. | Board-level or batch-level records that can connect components, process parameters, inspection results, and rework history. | Blank traceability report, retention policy, barcode workflow, and sample nonconformance record. | 5% |
| Quality system and workmanship | Assess documented quality procedures, operator training, defect handling, and workmanship criteria. | Current quality certification where required, trained inspectors, controlled work instructions, and acceptance criteria aligned with the purchase specification. | Certificate copies, training matrix, inspection standards, internal-audit summary, and corrective-action reports. | 4% |
| Prototype-to-production transition | Review the supplier’s process for design-for-manufacturing feedback, pilot builds, and production release. | Formal review of BOM, placement data, drawings, stencil, test points, panelization, and approved first article before volume production. | New-product-introduction checklist, sample DFM report, first-article report, and engineering-change process. | 3% |


 Close