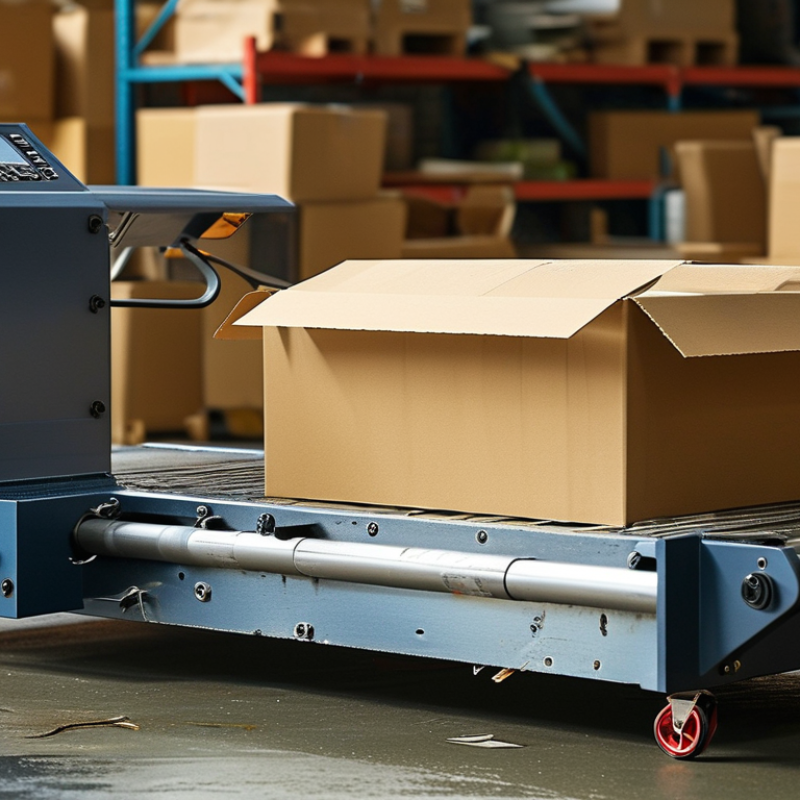
| Detection Principle | A transmitter coil generates an alternating electromagnetic field. A receiver system detects changes caused by conductive metal passing through the aperture. | Metal contamination inside sealed cartons, packs, or products can be detected without opening the package. | Confirm that the detector uses a balanced-coil or equivalent industrial detection architecture suitable for conveyor operation. |
| Detectable Metals | Ferrous metals, non-ferrous metals such as aluminum and copper, and stainless steel can be detected. Stainless-steel sensitivity is commonly lower than ferrous sensitivity. | Useful for finding broken blades, wires, screws, staples, machine fragments, and metal particles introduced during packing or handling. | Request separate test results for ferrous, non-ferrous, and stainless-steel contaminants rather than relying on one sensitivity figure. |
| Typical Test-Sphere Range | Many industrial systems are validated with test spheres approximately 0.8–3.0 mm in diameter, depending on aperture size, product effect, speed, and detector design. | Smaller apertures and stable, dry products generally allow better sensitivity than large apertures or products with strong electrical conductivity. | Use certified test pieces and record the tested metal type, sphere diameter, product position, and conveyor speed. |
| Operating Frequency | Industrial product metal detectors commonly use selectable frequencies from tens of kilohertz to several hundred kilohertz; some systems use multi-frequency operation. | Frequency selection helps balance sensitivity for different contaminant types and reduces the influence of the product being inspected. | Choose a system with frequency settings appropriate for carton contents, moisture level, salt content, foil packaging, and line speed. |
| Aperture Size | Typical conveyor apertures range from approximately 200–800 mm in width and 100–400 mm in height, although custom dimensions are common. | The carton must pass through the aperture with adequate clearance while avoiding an unnecessarily large opening that may reduce achievable sensitivity. | Specify the maximum carton width, height, orientation, and required safety clearance before selecting the detector head. |
| Conveyor Speed | Many packaging-line applications operate around 10–60 m/min. The actual limit depends on detector response time, carton spacing, and reject equipment. | The detector must identify the contaminated carton and trigger the reject device at the correct downstream position. | Verify detection performance at the highest planned production speed, not only during slow-speed testing. |
| Product Effect | Moisture, salt, temperature, density changes, and conductive packaging materials can create an electrical signal similar to a metal signal. | Cartons containing wet food, liquid-filled packs, foil, or high-salt products may be more difficult to inspect than dry paperboard products. | Run product-specific learning or auto-phase setup using representative cartons from the actual production process. |
| Reject Methods | Common mechanisms include air blast, pneumatic pusher, drop flap, diverter arm, and stop-and-remove systems. | The reject device removes the suspected carton without damaging adjacent cartons or interrupting the complete production line. | Match the reject method to carton weight, spacing, speed, allowable product loss, and available compressed air. |
| Detection Response | Industrial systems typically provide an electronic detection signal followed by a configurable delay and reject duration. | The delay compensates for the distance between the detector aperture and the reject point. | Validate timing with the fastest line speed and the smallest carton gap to prevent wrong-product rejection. |
| Reject Confirmation | Options may include a reject-bin sensor, air-pressure monitoring, flap-position feedback, and a second-pass verification sensor. | Confirmation helps identify blocked reject bins, failed pneumatic action, or cartons that were not successfully removed. | For critical applications, use reject confirmation with an alarm, line stop, or controlled quarantine procedure. |
| Ingress Protection | IP65 is commonly used for protected industrial environments; IP66, IP67, or IP69K may be selected for frequent washdown areas when properly specified. | Paperboard lines may produce dust, while food-packaging lines can require water-resistant construction and hygienic cleaning procedures. | Check the protection rating of the detector head, conveyor, control cabinet, sensors, and reject assembly as a complete system. |
| Electrical Supply | Industrial conveyor detectors commonly use single-phase supplies such as 100–240 V AC, 50/60 Hz, or a site-specific equivalent. | Stable power supports consistent detector operation and reliable communication with the conveyor control system. | Confirm voltage, frequency, rated current, grounding, isolation, and required control signals before installation. |
| Control Interfaces | Common interfaces include digital input/output, relay contacts, Ethernet-based communication, and industrial fieldbus options. | The detector can exchange running, fault, detection, reject, and line-stop signals with a programmable logic controller. | Define the required I/O points and communication protocol during line-design review. |
| Environmental Temperature | Many standard industrial systems are designed for approximately 0–40°C, while wider temperature ranges may be available for special environments. | Temperature changes can affect electronic stability and product characteristics, especially in chilled or heated packaging areas. | Check the specified operating range and allow the detector to reach stable operating conditions before validation. |
| Calibration and Testing | Routine performance checks commonly use certified metal test pieces at defined intervals, such as start-up, product changeover, and scheduled quality checks. | Testing demonstrates that the complete detection and rejection process remains effective during production. | Maintain records of test results, product code, line speed, test-piece size, operator, and corrective action. |
| Installation Factors | Vibration, nearby motors, variable-frequency drives, metal structures, poor grounding, and product accumulation can affect performance. | Mechanical and electrical interference may cause false alarms or reduce stable sensitivity. | Install the system on a rigid frame, separate it from strong interference sources, and follow the equipment grounding requirements. |
| Carton Spacing | Required spacing depends on carton length, conveyor speed, detector response, and reject timing; a defined gap is necessary for reliable separation. | Insufficient spacing can cause two cartons to be treated as one detection event or can interfere with accurate rejection. | Determine the minimum gap during a full-speed trial with the actual carton dimensions. |
| Compliance Considerations | Industrial equipment may need to meet applicable electrical safety, electromagnetic compatibility, machinery safety, and food-industry requirements. | Compliance supports safe integration into automated packaging lines and customer quality systems. | Request the applicable declarations, test documentation, user manuals, and validation procedures for the target market. |


 Close