7 Thermal Bond Non Woven Buying Tips for Global Buyers
Global buyers are paying closer attention to thermal bond non woven materials. Performance now matters as much as price.
Smithers’ The Future of Global Nonwovens to 2029 estimates continued growth across hygiene, filtration, medical, automotive, and construction applications. Grand View Research also reported strong expansion in the global nonwoven fabrics market. These figures reveal opportunity, but they hide procurement risk. Reported market values differ because definitions, regions, and product categories vary.
That detail matters.
Dr. Behnam Pourdeyhimi, a leading nonwoven materials researcher, describes nonwovens as “engineered materials.” His point is practical. Thermal bonding changes fiber structure, strength, softness, thickness, and thermal stability. A sample may look acceptable under warehouse lighting, yet fail after compression, washing, or heat exposure.
Experienced buyers inspect more than a data sheet. They compare fiber composition, basis weight, bonding temperature, tensile strength, elongation, air permeability, and shrinkage. They also request production-lot samples, not only showroom swatches. A roll with uneven edges can signal tension problems. A sharp odor may indicate processing or storage issues.
The seven buying tips in this guide connect laboratory data with factory reality. They address specifications, supplier audits, testing, certifications, logistics, pricing, and consistency. Some recommendations require extra time. That can feel inefficient.
However, a cheaper roll is not always a cheaper purchase.
One limitation deserves honesty: public industry reports rarely isolate Thermal Bond Non Woven products consistently. Buyers should verify every market claim with supplier records, independent testing, and application-specific trials. That disciplined approach supports better decisions across unfamiliar global supply chains.
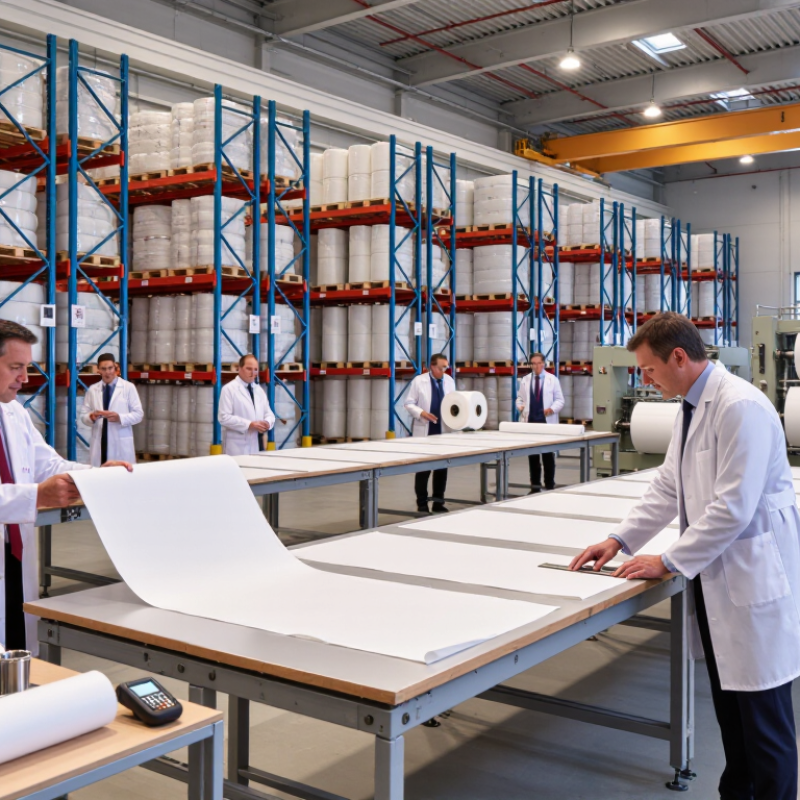
Define Thermal Bond Nonwoven Material Requirements
Define Thermal Bond Nonwoven Material Requirements
Before requesting quotations, define the fabric at the production level. Specify fiber type, blend ratio, basis weight, thickness, width, and roll length. For example, a 40–80 gsm polypropylene web may suit lightweight filtration, while thicker polyester structures provide stronger cushioning. Do not describe material as “soft” or “strong” alone. Those words invite inconsistent interpretations.
According to EDANA’s 2023 industry statistics, European nonwoven production reached roughly 3.1 million tonnes. This scale shows why small specification gaps can create major purchasing risks. State tensile strength in both machine and cross directions, elongation, air permeability, pore size, and thermal shrinkage. Add bonding temperature and maximum service temperature when heat exposure matters. A sample should be tested after conditioning, not only when freshly produced.
Smithers’ The Future of Nonwovens to 2028 identifies hygiene, filtration, and medical applications as important growth areas. Each requires different controls. Absorbent products may need liquid strike-through and retention data. Filtration materials need pressure-drop and efficiency results. Ask for test methods, laboratory conditions, and certificate dates. ASTM, ISO, or EN methods improve comparison, but they do not replace application trials. That part is often underestimated. A material can pass a laboratory test and still fail during high-speed converting. Define acceptable defects, splice limits, packaging, and storage humidity before approval. Recheck them after the first production shipment.
Thermal Bond Nonwoven Material Requirements
Buying tip: Select a binder fiber whose activation window matches the web-forming process, oven temperature, dwell time, and heat resistance of the carrier fiber. PE-sheath systems generally bond at lower temperatures, while PET-based systems require higher thermal settings.
The ranges shown are representative technical ranges for common binder-fiber systems, not brand-specific specifications. Actual bonding temperature depends on fiber denier, sheath composition, web density, line speed, pressure, and equipment configuration. Confirm the final setting through supplier data and production trials.
Compare Fiber Types, Web Structures, and Bonding Methods
Thermal bond nonwovens depend on fiber selection, web design, and heat control. INDA and EDANA reported global nonwoven production above 14 million tonnes in 2022. That scale hides major performance differences. PET offers stiffness and heat resistance. PP provides low density and chemical resistance. Bicomponent fibers can create a lower-melting sheath around a stronger core. This structure supports bonding without fully melting the web.
Tip: Match the fiber to the end use. A carded web suits uniform thickness and controlled orientation. An airlaid web gives a softer, more random structure. Spunlaid webs can improve strength and production speed. Do not choose by fiber price alone. Basis weight, crimp, and fiber length can change handling and final strength.
Tip: Compare bonding methods under real conditions. Point calendaring creates firm bonding points and a smoother surface. Through-air bonding gives better loft and softness. Excessive heat can flatten pores and reduce absorbency. Smithers’ recent nonwovens analysis identifies hygiene, filtration, and medical applications as important demand areas, where breathability and consistency matter. Test tensile strength, thickness, air permeability, and shrinkage after heat exposure.
Tip: Request production evidence. Ask for basis-weight tolerances and bonding-temperature ranges. Review samples from the machine edges, not only the center. A perfect laboratory sheet may fail during high-speed converting. This is an easy detail to miss. Small differences in web uniformity can become visible defects in the finished roll.
Verify Samples Before Finalizing a Global Purchaseҵан
Before finalizing a global thermal bond nonwoven purchase, verify physical samples from the actual production lot. A catalog sheet cannot reveal every handling problem. Request samples matching the proposed basis weight, thickness, width, and fiber blend. Test them under normal use conditions. Test them twice.
Measure tensile strength in both machine and cross directions. Check elongation, softness, surface uniformity, and thermal shrinkage after controlled heating. A simple visual check can reveal loose fibers, uneven bonding, edge curl, or dark specks. Measure the sheet at several points, not only the center. Edges often behave differently.
Ask for samples from more than one roll. Compare results with the supplier’s technical data and your internal specifications. If possible, let operators run the material through your real cutting, folding, or lamination process. Record dust, static, tearing, and feeding resistance. Small issues become expensive when production runs continuously. Confirm roll diameter, core size, moisture protection, labels, and export packaging before approval.
Do not rely on one perfect sample. It may have received extra inspection or better storage. I have seen materials pass a hand test but fail after humidity exposure. That gap deserves attention. Keep an approved reference sample, signed test records, and clear acceptance limits. If the sample differs from mass production, pause the order and investigate the cause. Supplier explanations matter, but measured evidence matters more.


 Close

