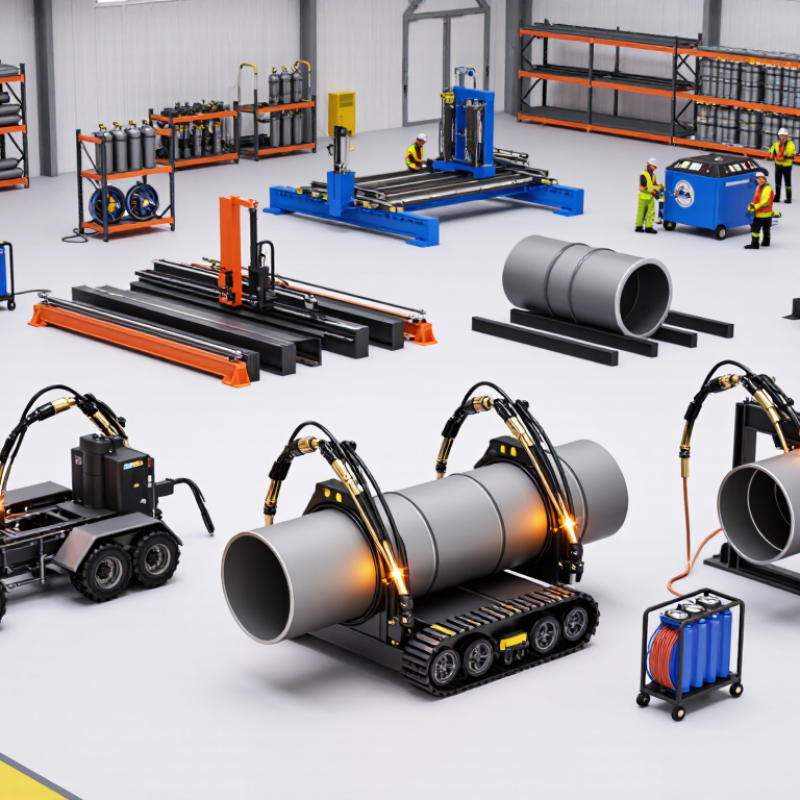
| 1 | Dual-Torch GMAW Pipeline Buggy | Gas metal arc welding (GMAW) | Two tandem torches mounted on a mechanized carriage | 16–48 in (406–1,219 mm) | 6–20 mm | 0.25–0.90 m/min | Constant-voltage inverter, typically 300–500 A per torch | Onshore transmission pipelines and long straight welds | High deposition rate with consistent travel speed |
| 2 | Dual-Torch FCAW Pipeline System | Flux-cored arc welding (FCAW) | Leading and trailing torches positioned along the same weld path | 20–56 in (508–1,422 mm) | 8–25 mm | 0.20–0.75 m/min | Constant-voltage inverter, typically 350–550 A per torch | High-strength steel transmission and gathering lines | Strong penetration and good productivity in outdoor work |
| 3 | Dual-Torch GMAW/FCAW Combination Machine | GMAW root or hot pass with FCAW fill and cap | One torch dedicated to the front pass and one to fill or cap work | 24–60 in (610–1,524 mm) | 10–30 mm | 0.18–0.65 m/min | Two independent inverter power sources | Large-diameter cross-country pipelines | Combines controlled root welding with high-rate filling |
| 4 | Dual-Torch Tandem GMAW Machine | Tandem gas metal arc welding | Two wire electrodes arranged in tandem with a controlled arc distance | 24–60 in (610–1,524 mm) | 8–22 mm | 0.35–1.20 m/min | Dual-pulse or tandem GMAW power system, up to about 600 A per torch | High-volume pipeline construction and repeatable girth welds | Very high deposition rate and reduced cycle time |
| 5 | Dual-Torch GTAW Root-Pass Machine | Gas tungsten arc welding (GTAW/TIG) | Two GTAW torches operating on opposite or sequential sections | 8–36 in (203–914 mm) | 3–12 mm | 0.05–0.25 m/min | Constant-current power sources, typically 150–300 A per torch | Stainless steel, alloy steel, and demanding root passes | Excellent arc control and high-quality root penetration |
| 6 | Dual-Torch Orbital TIG Pipeline Welder | Orbital GTAW with controlled wire feeding | Two torches travel around the pipe on a synchronized orbital track | 2–24 in (51–610 mm) | 1.5–10 mm | 0.03–0.18 m/min | Programmable constant-current inverter, typically 100–250 A per torch | Process piping, sanitary lines, and precision tube-to-pipe joints | Repeatable weld profiles on small and medium diameters |
| 7 | Dual-Torch Submerged Arc Welding Machine | Submerged arc welding (SAW) | Two submerged arc heads positioned in tandem on an external track | 30–72 in (762–1,829 mm) | 12–40 mm | 0.30–1.00 m/min | Two constant-voltage SAW power sources, commonly 600–1,200 A per torch | Fabricated pipe mills and thick-wall pipeline sections | Deep penetration and high deposition with minimal arc glare |
| 8 | Dual-Torch Internal Line-Up Welding Machine | Mechanized GMAW or FCAW | Two torches mounted on an internal welding head or internal clamp | 20–56 in (508–1,422 mm) | 6–22 mm | 0.20–0.80 m/min | Portable inverter systems, typically 300–500 A per torch | Field girth welding where internal access is available | Accurate root alignment and reduced external setup time |
| 9 | Dual-Torch External Track Welding Machine | Mechanized GMAW, FCAW, or hybrid arc welding | Two torches travel around the outside of the pipe on a rigid track | 24–60 in (610–1,524 mm) | 8–28 mm | 0.15–0.70 m/min | Two synchronized inverter power sources, typically 300–550 A per torch | Repair, tie-in, and field girth welds | Fast installation and flexible access for field operations |
| 10 | Dual-Torch Hot-Wire TIG Pipeline Machine | GTAW with hot-wire filler metal | One torch creates the arc while a second torch or hot-wire circuit preheats filler wire | 12–36 in (305–914 mm) | 6–20 mm | 0.10–0.45 m/min | Constant-current TIG source with a separate hot-wire power unit | Corrosion-resistant, alloy, and high-integrity pipeline welds | Higher TIG deposition without sacrificing weld cleanliness |


 Close