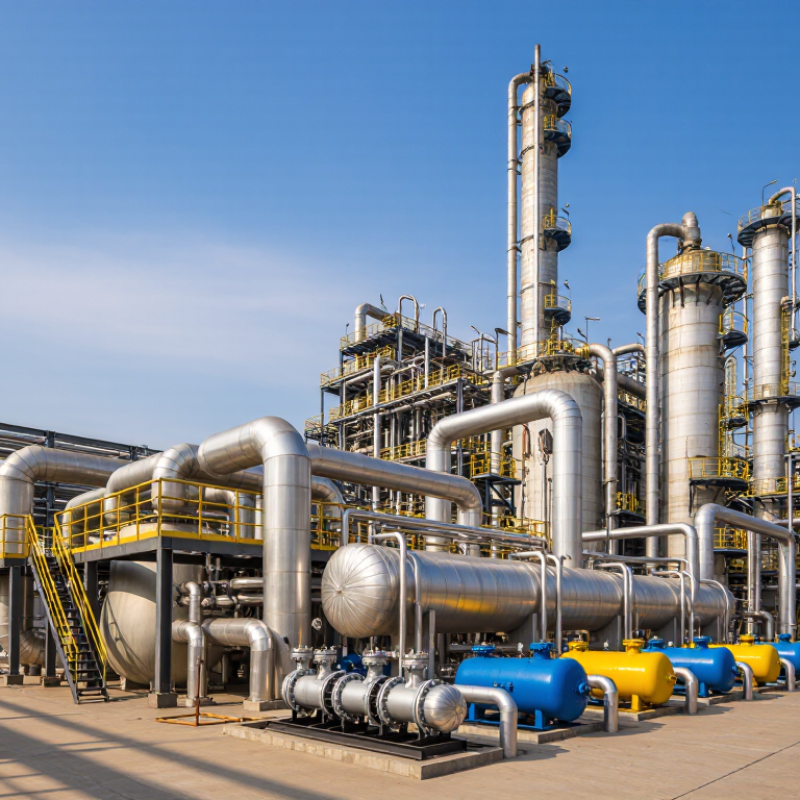
| Process Reactors | Stirred-tank reactors, tubular reactors, and batch reactors | Provide controlled conditions for chemical reactions, including temperature, pressure, mixing, and residence time. | Polymer production, pharmaceuticals, specialty chemicals, and fertilizer processing | Reactor design affects reaction control, product consistency, throughput, and safe handling of heat and pressure. |
| Heat Exchangers | Shell-and-tube, plate, and air-cooled heat exchangers | Transfer heat between process streams while keeping the fluids separated in most designs. | Heating, cooling, condensation, and heat recovery in chemical plants and refineries | Efficient heat transfer supports process temperature control and can reduce energy use. |
| Separation Equipment | Distillation columns, absorbers, strippers, and evaporators | Separate or concentrate components using differences in volatility, solubility, or other physical properties. | Petrochemicals, solvents, gas treatment, and production of purified chemical products | Separation equipment helps achieve required product purity and recover valuable materials from process streams. |
| Pumps and Compressors | Centrifugal and positive-displacement pumps; centrifugal and reciprocating compressors | Move liquids or increase the pressure of gases through a process system. | Liquid transfer, pipeline service, gas processing, and plant utility systems | Reliable flow and pressure control are essential for continuous operation and stable process conditions. |
| Pressure Vessels | Reactors, separators, accumulators, and storage vessels designed for pressure service | Contain gases or liquids at pressures different from the surrounding atmosphere. | Chemical processing, gas handling, and high-pressure reaction systems | Appropriate design, materials, fabrication, and inspection help manage pressure-related hazards. |
| Filtration and Solid-Liquid Separation | Filter presses, cartridge filters, bag filters, and centrifuges | Remove suspended solids from liquids or separate solids from liquids or slurries. | Fine chemicals, water treatment, catalyst recovery, and product finishing | These systems help meet product-quality requirements and support recovery or safe disposal of process solids. |
| Storage and Handling Equipment | Storage tanks, silos, hoppers, and loading systems | Store and transfer liquids, powders, and bulk materials between process stages. | Raw-material storage, intermediate products, finished chemicals, and plant logistics | Properly selected storage and handling equipment helps protect materials and reduce spills, contamination, and exposure risks. |
| Mixing and Agitation Equipment | Agitators, industrial mixers, and blending systems | Combine materials and promote uniform temperature, concentration, or particle distribution. | Formulation, dissolution, blending, and reaction processes | Effective mixing can improve product uniformity and help maintain predictable process performance. |



 Close